
Adhesive Coat Weight in gsm: What Your Label Stock Really Carries
Short answer: adhesive coat weight is the dry mass of glue per square metre of label stock, quoted in grams per square metre. General-purpose permanent acrylic sits at 18–22 gsm; film and low-surface-energy work at 22–28 gsm; removable constructions at 10–15 gsm. A buyer can verify a delivery without a coating lab: cut 100 cm² of laminate, weigh it on a 0.001 g balance, strip the adhesive, weigh again, and multiply the difference by 100. Do that at three lanes across the web and three positions along the roll, because a batch passes on its average and fails on its profile.
Most disputes about adhesive coat weight are not disputes about adhesion at all. They are disputes about which number was quoted, on which method, at which point on the web. A roll that reads 20 gsm on the certificate and 17 gsm at one edge is not a lie on paper; it is an average doing what averages do. The practical job is to know what the number controls, and to test the part of it that a datasheet cannot show you.
What coat weight measures, and the three things it does not
Coat weight is mass, not thickness. Dry adhesive density sits close to 1.0–1.1 g/cm³, so 20 gsm works out to roughly 18–20 microns of glue, and the difference between an 18 gsm and a 22 gsm construction is about four microns — thinner than a human hair and almost invisible on a cross-section photograph. That four microns is also the difference between a kiss-cut that strips cleanly and a blade that smears.
It is always a dry figure. Water-based acrylic is typically applied at 40–50% solids, so the wet coat on the head is two to two and a half times the dry number on the technical data sheet. When one quotation looks dramatically heavier than every other quotation for the same job, the usual explanation is that one of them is wet. Ask which one before you compare price per square metre.
Coat weight also says nothing about chemistry. A 20 gsm rubber-based hot melt and a 20 gsm crosslinked acrylic are the same mass and behave nothing alike in a 45 °C warehouse. Nor does the average say anything about profile. Two rolls can both certify 20 gsm while one is flat across its width and the other swings between 16 and 24 gsm edge to edge; the first runs for a month, the second blocks in the top layer of a pallet and passes every peel test taken from the lead edge.
The last thing the number does not cover is the liner. A 100 cm² coupon of finished laminate is mostly backing paper: a 62–80 gsm glassine liner outweighs the adhesive by three to four times. Any check that weighs the whole construction and calls the result “coat weight” is really measuring total grammage — useful for catching a substitution, useless for judging glue mass until the face and liner are subtracted. The grammage ranges and how they interact with dispensing are set out on the glassine liner page.
The four windows we quote, and where each one fails
Coat weight is chosen by the substrate and by the failure you are trying to avoid, not by a wish for something stronger. The windows below are the ones we run on a 1080 mm web; treat the boundaries as engineering choices rather than as limits written into any standard.
| Dry coat weight | What it is for | Usual face | Where it fails first |
|---|---|---|---|
| 10–15 gsm | Removable and repositionable labels, promo and mailer stock, surfaces that get wiped down | Coated paper, white BOPP | Edge lift on curved glass above 60 °C; residue if the dwell is long |
| 18–22 gsm | General permanent work: retail, logistics, thermal shipping labels, cartons | Coated paper, thermal paper, white BOPP | Rough recycled corrugate and low-energy plastics, where contact area is the limit |
| 22–28 gsm | Film labels on squeeze and curved packs, chilled and frozen goods, condensation | BOPP, PE, PET | Blocking in a hot store; ooze at the slit edge of tightly wound rolls |
| 28–35 gsm | Textured or fibrous surfaces, high-tack low-surface-energy work, cold application | PE, PP, vinyl, technical films | Adhesive stringing at the die, blade cleaning stops, contour cut bleed |
Two entries in that table deserve a warning. The 22–28 gsm band is where buyers most often ask for “one step heavier” to fix a lifting label on a squeeze bottle, and it is the band where extra mass helps least: on a PE bottle at 31 dyn/cm, the adhesive never wets out properly no matter how much of it you apply. The 28–35 gsm band is where die-cutting complaints originate, because a soft heavy coat deforms under the blade instead of fracturing cleanly.
Verifying a delivery with a balance and a knife
A coat weight check needs less equipment than most buyers assume: a cutting template, a sharp blade, a balance, and a solvent for the adhesive. What it needs more of is discipline about the sample size, because the arithmetic is unforgiving at small areas.
Take 100 cm² — 100 mm by 100 mm, cut with a die or a steel template rather than by eye. That coupon carries 0.01 m² of material, so each 0.01 g of balance resolution equals one full gram per square metre of error. A balance that reads to two decimal places is therefore blind to exactly the drift you are trying to catch: a nominal 20 gsm roll that is really running 19 gsm shows the same reading. Either move to a 0.001 g balance, which resolves 0.1 gsm at this area, or cut 500 cm² and keep the cheaper balance, which resolves 0.2 gsm.
Condition the coupon before weighing. Storage bulletins from the main material makers cluster around 20–25 °C and 40–60% relative humidity, and paper picks up or loses moisture fast enough to move a 100 cm² coupon by more than the tolerance you are testing. Thirty minutes on a bench in the QC room is enough for a thin coupon; a roll straight off a container after three weeks at sea is not.
For a paper-faced laminate, stripping the adhesive cleanly is not realistic — the solvent takes the fibre with it. The workable procedure is a two-part one. First weigh the whole construction and compare against the sum of face, adhesive and liner grammage on the technical data sheet; a shortfall of 3 gsm on a 200 gsm construction shows up as 0.03 g on a 100 cm² coupon, which is exactly why the balance resolution matters. Second, keep one film-faced sample of the same batch — PET or BOPP — where the adhesive can be washed off and weighed directly. The film sample is the one that produces a defensible number.
Sampling is where most incoming inspections fail. Nine coupons is the minimum useful set: three lanes across the 1080 mm width, taken near each edge and at the centre, repeated at the head, middle and tail of the roll. Log the nine readings rather than the mean. If the mean is 20.1 gsm and the spread is 18.4 to 21.9, the roll is not a 20 gsm roll; it is a roll that will block on one side of the pallet and die-cut differently on the other.
Why a heavier coat is not a stronger label
Adhesion is a surface-energy problem before it is a mass problem. Below roughly 36–38 dyn/cm, a standard permanent acrylic cannot wet a surface out; PP sits near 29 dyn/cm and PE near 31, both well under the threshold, and adding four grams of the same glue to a PE bottle buys mass without buying contact. The fix at that point is chemistry — a modified acrylic, a softer base, a primer — not volume. The substrate-by-substrate logic is on the adhesive selection matrix.
Above the right weight, the failure modes change sign. Extra adhesive squeezes sideways under winding tension, so the slit edge goes tacky and adjacent layers fuse: blocking. In a warehouse at 20–25 °C that may never appear; on the top rack of a container, or in a store room that reaches 45 °C in August, a coat at the top of its window is the first thing to move. The same surplus softens under the die, and a blade that should fracture the adhesive film starts dragging it — a symptom usually blamed on the die, documented on the laser die-cutting page.
| What you see | What the number is doing | Change this first |
|---|---|---|
| Edge lift within hours on a curved pack | Mass is adequate, wet-out is not: the surface is under 36 dyn/cm | Adhesive family, not gsm |
| Roll edges tacky, layers fused after weeks in store | Coat parked at the top of the window, adhesive too soft for the climate | Trim 2–3 gsm, or raise crosslink density |
| Blade needs cleaning every half hour | Heavy soft coat deforming instead of fracturing at the die | Coat weight and kiss-cut depth together |
| Peel passes on the lead edge, fails mid-roll | Average fine, profile drifting along the length | A nine-point batch record, not a new supplier |
What one gram does across 1080 mm at 180 m/min
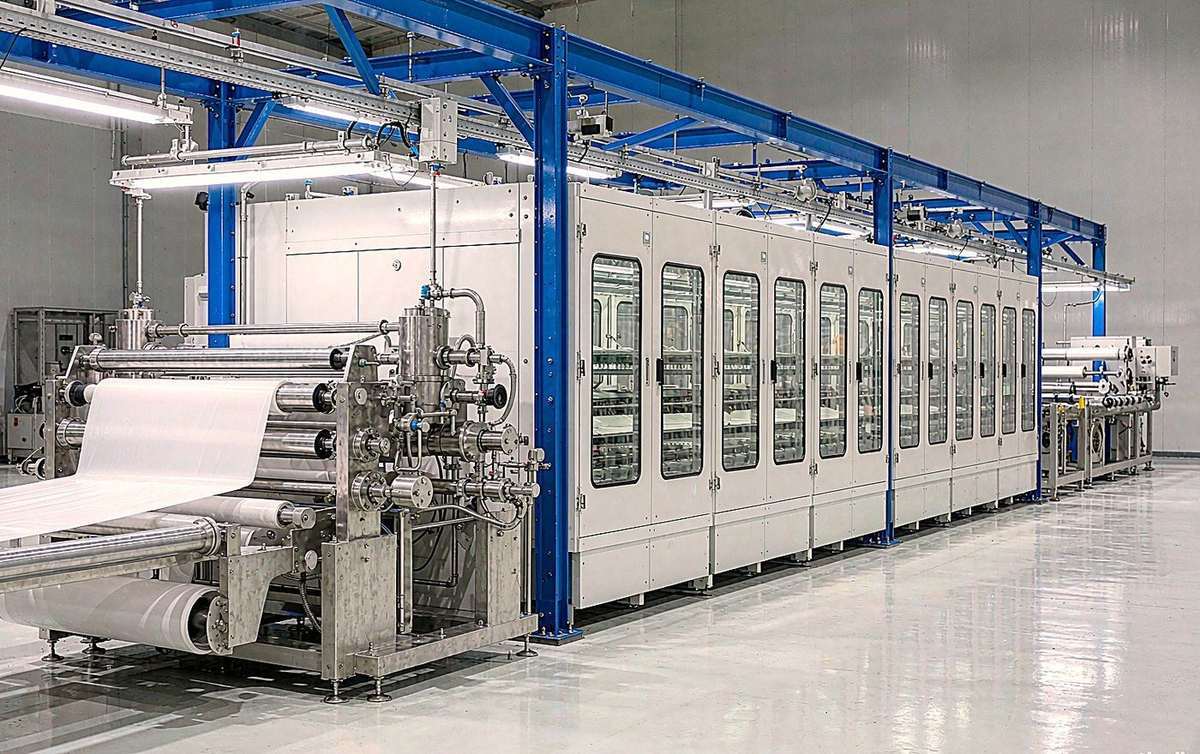
Our coating width is 1080 mm and the line runs at 180 m/min, which together set the practical limits of the number. A wide web gives room for a lot of sellable width, and it also gives a head more chances to drift: the same percentage error at the operator side and the drive side produces two different materials in the same roll. At 180 m/min the web crosses the drying section in seconds, so the weight has to be right at the head. There is no downstream correction, only a batch record that tells you what actually left the plant.
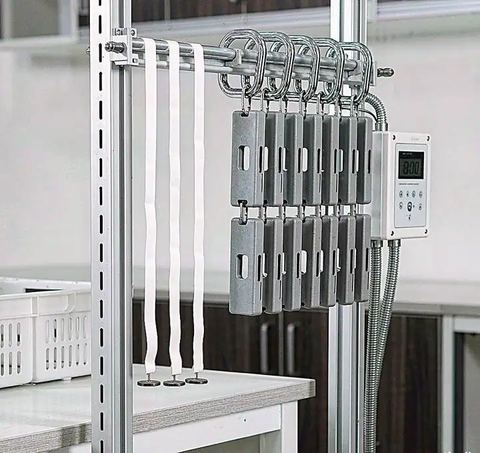
That is why each batch gets five checks rather than one. Initial tack by rolling ball, holding power under shear, 180° peel, climate ageing, and a visual pass on coating appearance. They are not interchangeable, and they do not respond to coat weight in the same way: tack is dominated by chemistry and barely moves with two extra grams, peel is a mixed signal of mass and wet-out, while holding power is the test that tracks mass most closely, because shear resistance scales with the volume of adhesive carrying the load. A batch that reads light on the balance usually shows it in shear before anywhere else.
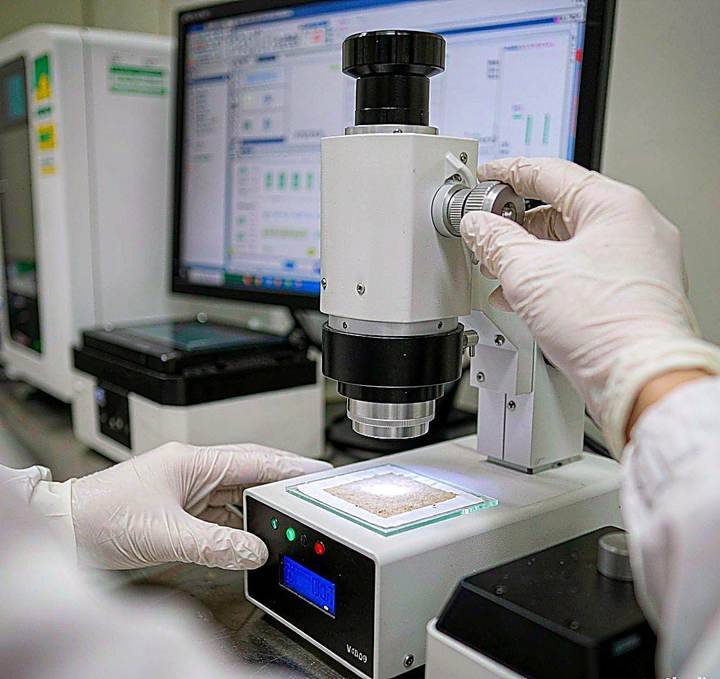
The visual check catches what the balance cannot. Streaks, uncoated lanes and a matte band down one side are all profile failures that a single coupon will never reveal, because the coupon may simply not come from the bad lane. Examined under magnification, the difference between a uniform adhesive film and one with a dry lane is obvious in seconds, and it correlates with the die-cutting and blocking complaints that arrive weeks later.
Peel and ageing answer different questions again. Peel is where the test conditions matter more than most buyers expect — the same laminate reads differently on steel and on glass, and differently at 300 mm/min than at 100 — which is why the numbers only compare when the conditions are quoted alongside them, as set out in the peel test conditions note. Ageing is the check that exposes a coat sitting just inside its window: seven days at elevated temperature will push a marginal roll into ooze while a correctly trimmed one stays put.
Writing coat weight into the purchase order
The specification line that prevents most of these arguments is short, and it is about method as much as number: “Permanent acrylic, dry coat weight 20 gsm ±1 gsm, measured gravimetrically at three positions across the web and three along the roll, batch record supplied with the shipment.” That sentence forces the supplier to say whether the figure is dry, to commit to a tolerance, and to hand over nine readings instead of an average. A tolerance clause without a sampling rule is only decoration.
Ask what the target is worth in volume before trading on it. The minimum order is 1,000 m², which at 1080 mm width is about 925 linear metres, and production runs 15–25 days before sea freight. On that quantity, four extra grams of adhesive is four kilograms of dry solids — a small line on any invoice, and a poor reason to accept a coat that blocks in transit. The money is not in the glue; it is in the roll that cannot be unwound on a Friday afternoon.
Two documents are worth insisting on beyond the data sheet. The batch coat weight record, because it is the only evidence of the material you actually received rather than the material that was designed. And a profile statement, edge to centre to edge, because a wide web is exactly where an average hides a lane. Buyers who ask for both tend to discover their coating problems at goods-in rather than at the customer's line; the formats we supply are listed with the material families on the product pages, and the line capability behind them is on technology.
A certificate that carries nine readings across the width is a stronger acceptance document than any datasheet average, and it costs nothing to ask for before the roll ships. The alternative is learning the profile one complaint at a time.
FAQ
Is 20 gsm of adhesive the same as 20 microns of adhesive?
No, though the two numbers sit close enough to be confused. Dry adhesive density is roughly 1.0 to 1.1 grams per cubic centimetre, so 20 gsm works out to about 18 to 20 microns of dry film, and the gap widens as density rises. When a supplier quotes microns, ask whether that figure is dry film or wet coat: a water-based acrylic applied at 45 percent solids is more than twice as thick at the head as it is once the water is gone.
Can I check coat weight with a 0.01 g balance?
Only if you cut a larger coupon. At 100 square centimetres, 0.01 g of resolution equals one full gram per square metre of error, which is the entire tolerance on a 20 gsm target. Cut 500 square centimetres and the same balance resolves about 0.2 gsm; keep the 100 square centimetre coupon only if the balance reads to 0.001 g. Condition the coupon at around 23 degrees Celsius and 50 percent relative humidity first, because paper moves with moisture faster than the tolerance you are testing.
Does a heavier coat weight give higher peel adhesion?
Up to a point, and the point arrives earlier than most buyers expect. Peel depends on wet-out, dwell time and adhesive chemistry as much as on mass, so on a PP surface near 29 dyn/cm or a PE surface near 31 dyn/cm extra grams buy nothing until the adhesive itself changes. Past the useful window the surplus shows up as edge ooze, blocking in a hot store and adhesive build-up on the die.
What tolerance should I accept on a 20 gsm target?
Plus or minus 1 gsm is a realistic ask on a single-pass coating line, but the tolerance is worth less than the sampling rule attached to it. Specify three positions across the web and three along the roll, and ask for the nine readings with the batch record. A tight average with a four gram spread from edge to centre still leaves you one lane that behaves like a different material.
Will coat weight affect die-cutting and dispensing?
Yes, and usually before it affects adhesion. A soft coat parked at the top of its window deforms under the blade instead of fracturing, so the waste matrix does not strip cleanly and the blade needs cleaning far more often. On the applicator the same surplus migrates to the peel plate and the sensors. Trimming two grams per square metre frequently settles a die-cutting complaint that was being treated as a mechanical fault.